As a trusted supplier of the R1 - 200, I am frequently asked about the certifications that this remarkable product holds. In this blog, I'll delve into the various certifications of the R1 - 200, shedding light on why they matter and what they signify for our customers.
CE Certification
The CE mark is a crucial certification for the R1 - 200. CE stands for Conformité Européene, which translates to European Conformity. This certification indicates that the R1 - 200 meets all the essential health, safety, and environmental protection requirements set by the European Union.
The CE marking process involves a series of strict tests and assessments. Our R1 - 200 has been evaluated for electrical safety, electromagnetic compatibility (EMC), and mechanical safety. For electrical safety, the product is tested to ensure that it does not pose any risks such as electric shock to the users. EMC testing is carried out to make sure that the R1 - 200 does not emit excessive electromagnetic interference that could disrupt other electronic devices. And in terms of mechanical safety, the product's structure and components are examined to prevent any potential physical hazards.
This certification is not only important for selling the R1 - 200 in the European market but also serves as a testament to the high - quality and safety standards of our product. When customers see the CE mark on the R1 - 200, they can have confidence that it has undergone rigorous testing and meets the strictest European regulations.
RoHS Certification
The Restriction of Hazardous Substances (RoHS) directive is another significant certification that the R1 - 200 possesses. RoHS restricts the use of six hazardous materials in the manufacture of various types of electronic and electrical equipment. These materials include lead, mercury, cadmium, hexavalent chromium, polybrominated biphenyls (PBBs), and polybrominated diphenyl ethers (PBDEs).
Our commitment to RoHS compliance means that the R1 - 200 is environmentally friendly. By eliminating these hazardous substances, we are not only reducing the impact on the environment but also ensuring the safety of our customers. For example, lead can be extremely harmful to human health, especially to the nervous system, and cadmium is a known carcinogen. By adhering to the RoHS directive, we are contributing to a greener and healthier world.
ISO 9001 Certification
ISO 9001 is an international standard for quality management systems. This certification shows that our company has a well - defined and effective quality management system in place for the production of the R1 - 200.
The ISO 9001 certification process involves a comprehensive audit of our company's operations, from product design and development to production, installation, and service. It ensures that we have processes in place to consistently meet customer requirements and enhance customer satisfaction. For the R1 - 200, this means that every step of the manufacturing process is carefully monitored and controlled. We have procedures for raw material inspection, in - process quality control, and final product testing.
This certification is a clear indication of our dedication to quality. It gives our customers the assurance that the R1 - 200 they purchase is of the highest quality and that we are committed to continuous improvement in our products and services.
Comparison with Similar Products
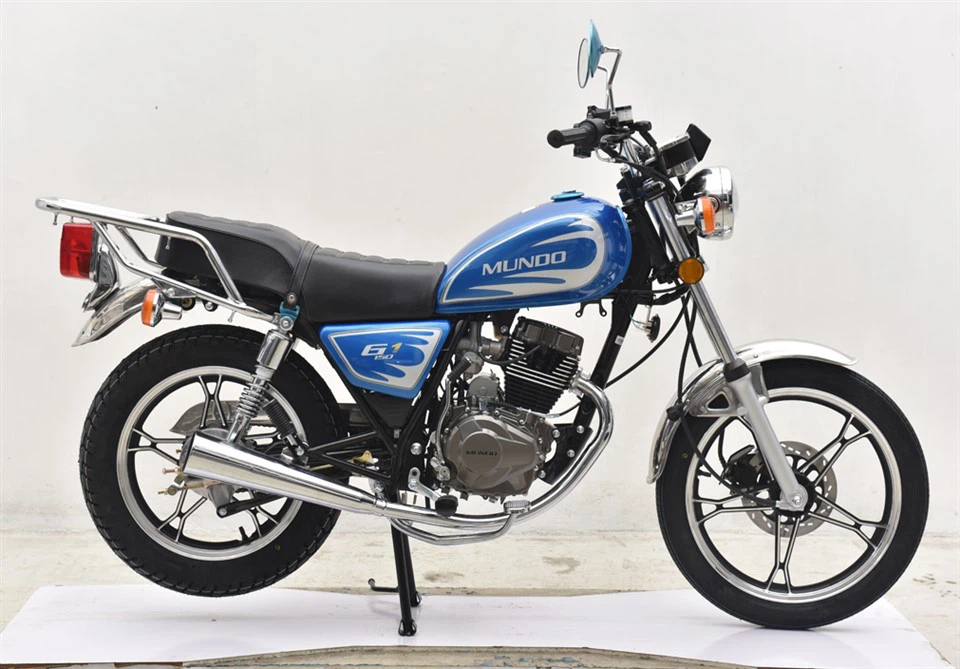
When comparing the R1 - 200 with other similar products in the market, such as the A2 - 200 and the G1 - 150, our product's certifications give it a distinct advantage. The CE, RoHS, and ISO 9001 certifications demonstrate that the R1 - 200 meets or exceeds the safety, environmental, and quality standards set by international regulations.
Many competing products may not have all these certifications, which could mean that they do not offer the same level of safety and quality. For example, a product without RoHS certification may contain hazardous substances that could be harmful to the environment and human health. And a product without ISO 9001 certification may not have a well - structured quality management system, leading to inconsistent product quality.
The Impact of Certifications on the Product's Performance
The certifications of the R1 - 200 are not just about meeting regulatory requirements; they also have a direct impact on the product's performance. The CE certification, with its focus on electrical safety and EMC, ensures that the R1 - 200 operates smoothly without any electrical glitches or interference. This means that users can rely on the product to perform consistently in different environments.
The RoHS certification, by eliminating hazardous substances, can also improve the long - term reliability of the R1 - 200. Hazardous substances can sometimes cause corrosion or other damage to the internal components of the product over time. By removing these substances, we are increasing the lifespan of the R1 - 200 and reducing the likelihood of malfunctions.
The ISO 9001 certification, with its emphasis on quality management, ensures that the manufacturing process is optimized for high - performance products. Every component of the R1 - 200 is carefully selected and tested, and the assembly process is carried out with precision, resulting in a product that performs at its best.
Customer Benefits
For our customers, the certifications of the R1 - 200 bring a multitude of benefits. Firstly, they provide peace of mind. Customers can be confident that they are purchasing a safe, reliable, and environmentally friendly product. Whether they are using the R1 - 200 for personal or professional purposes, they know that it has been thoroughly tested and meets international standards.
Secondly, the certifications can save customers money in the long run. A high - quality product like the R1 - 200 is less likely to break down, reducing the need for costly repairs or replacements. And because it is environmentally friendly, customers can also contribute to a sustainable future.
Industry Recognition
The certifications of the R1 - 200 have also earned us recognition in the industry. Our commitment to quality, safety, and environmental protection has made us a trusted name among our peers. Other companies in the industry often look to us as an example of how to produce high - quality products that meet international standards.
Our Future Plans
We are constantly looking for ways to improve the R1 - 200 and our overall product line. In the future, we plan to pursue additional certifications that will further enhance the product's performance and competitiveness. For example, we are considering obtaining UL (Underwriters Laboratories) certification, which is widely recognized in the United States and other countries for product safety.
Conclusion
In conclusion, the R1 - 200 holds several important certifications, including CE, RoHS, and ISO 9001. These certifications not only demonstrate the high - quality, safety, and environmental friendliness of our product but also have a positive impact on its performance and customer benefits. When compared to similar products like the A2 - 200 and the G1 - 150, the R1 - 200 stands out for its comprehensive certification portfolio.
If you are interested in purchasing the R1 - 200 or have any questions about our product, we encourage you to reach out to us for a procurement discussion. We are eager to work with you and provide you with the best - quality products and services.
References
- European Union CE Marking regulations
- RoHS Directive Documentation
- ISO 9001 Standard Documentation